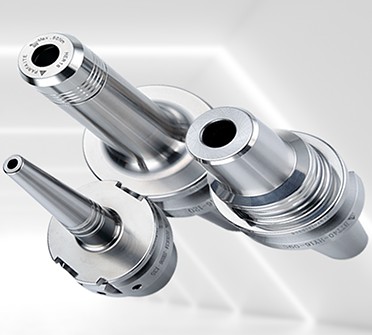
In modern CNC machining, the tool holder directly influences machining accuracy, surface finish, tool life, spindle performance, and overall production efficiency. Our complete tool holding portfolio includes ER Collet Chuck, Milling Chuck, Hydraulic Chuck, Shrink Fit Chuck, End Mill Holder, Face Mill Arbor, Drill Chuck Holder, Tapping Chuck, Boring System, and BT/CAT/SK/HSK Tool Holders.
Specification
- Tool Holder Interface: BT, CAT, SK, HSK, ISO, NBT
- Tool Clamping System: ER Collet, Milling Chuck, Hydraulic, Shrink Fit, Weldon
- Runout Accuracy: 0.003mm to 0.01mm depending on series
- Balancing Grade: Up to G2.5 at 25,000 RPM
- Coolant Options: Through Coolant / Peripheral Coolant
- Tool Diameter Range: 1mm to 50mm
- Material: Alloy Steel, Hardened and Precision Ground, HRC 54-60
Product Content
ER Collet Chuck offers wide clamping range and versatility for general machining. Milling Chuck delivers stronger gripping force for heavy milling. Hydraulic Chuck provides extremely low runout and damping for high-speed finish milling. Shrink Fit Chuck offers the highest rigidity and balance for aerospace and mold applications. End Mill Holder uses side-lock for rough machining. Face Mill Arbor mounts face milling cutters and shell mills. Tapping Chuck compensates synchronization errors for threading. Boring System provides fine diameter adjustment for precision bores. BT/CAT/SK/HSK series cover the main spindle interface standards used worldwide.
Which Tool Holder Should You Use?
Most tool holder complaints turn out to be selection problems rather than quality problems. A holder that is ideal for heavy roughing is the wrong choice for a finishing pass, and a high-precision holder will be destroyed by a cut it was never meant to take. Use the table below to narrow the shortlist, then confirm the exact series against the datasheets further down this page.
| Holder type | Typical runout (T.I.R.) | Clamping force | Vibration damping | Best suited to | Watch out for |
|---|---|---|---|---|---|
| ER Collet Chuck | around 0.01 mm | Medium | Low | General milling, drilling and tapping. Widest diameter coverage from a single holder. | Runout depends on the condition of the collet and nut. Worn collets are the usual cause of poor finish. |
| Milling Chuck | 0.005 to 0.01 mm | Very high | Medium | Heavy roughing and high radial load. | Large nose diameter can limit access around fixtures and walls. |
| Hydraulic Chuck | 0.003 mm or better | High | High | Finish milling, reaming and boring. High spindle speeds. | Requires a ground h6 shank. Not for side-lock flats or interrupted heavy cuts. |
| Shrink Fit Chuck | 0.003 mm or better | Very high | Low | 5-axis work, deep cavities, mould and die, high speed. | Needs an induction heater. One bore diameter per holder, so inventory grows. |
| End Mill Holder (Weldon) | Grip is the priority here, not runout | Very high, positive | Low | Heavy cuts where tool pull-out is the real risk. | The side screw offsets the tool. This is not a finishing holder. |
| Face Mill Arbor | Set by the cutter | – | – | Shell mills and face milling cutters. | The arbor pilot must match the cutter bore exactly. |
| Tapping Chuck | – | – | – | Tapping with length and torque compensation. | Choose rigid or compensating to match what the machine can synchronise. |
| Boring System | Fine adjustable | – | – | Precision bores held to close tolerance. | Balance becomes critical as speed rises. |
Hydraulic Chuck Specifications (BT, JIS B6339)
Figures below are taken from the current Hydraulic Chuck datasheet. Three body styles are available: Conventional (ADB-HC), Reinforced (AD and ADB-HCR) and Slim (ADB-HCS). Gauge lengths run from 58 mm to 150 mm depending on style, so reach can be matched to the job instead of over-hanging a standard holder.
| Item | BT30 | BT40 | BT50 |
|---|---|---|---|
| Clamping diameter | 6 – 20 mm | 3 – 32 mm | 6 – 32 mm |
| Run-out (T.I.R.) | 3 micron or less | 3 micron or less | 3 micron or less |
| Maximum speed | 25,000 rpm | 25,000 rpm | 20,000 rpm |
| Residual unbalance | 1 g.mm or less | 1 g.mm or less | 1 g.mm or less |
| Balancing grade | G2.5 to ISO 1940 | ||
| Tool shank tolerance | h6, for direct clamping without a sleeve | ||
| Taper standard | BT to JIS B6339 | ||
Spindle Interfaces: BT, CAT, SK and HSK
The interface is decided by your machine, not by preference, so this is usually the first thing to confirm before anything else on this page matters.
- BT (JIS B6339) – the Japanese standard, symmetrical flange, dominant across Asian-built machining centres.
- CAT (ANSI/ASME B5.50) – the North American standard. Same 7:24 taper as BT but a different retention knob and flange, so the two are not interchangeable.
- SK (DIN 69871) – the European standard, again 7:24 taper, widely used on German and Italian machines.
- HSK (DIN 69893) – a hollow short taper that contacts on both the taper and the flange face. Better rigidity and repeatability at high speed, which is why it dominates 5-axis and HSC work.
- ISO and NBT – also available where a machine calls for them.
Datasheets
- ER Collet Chuck (PDF) – dimensions and collet coverage
- Tool Holder Range (PDF) – AHC hydraulic, AMG double power, ASG / ASC milling chucks, SC straight collets
- MER Spring Chuck (PDF)
- All datasheets
Frequently Asked Questions
Which interface do I need – BT, CAT, SK or HSK?
Your machine decides. Check the spindle nose on the machine nameplate or manual. BT and CAT share the same 7:24 taper but use different retention knobs and flanges, so a BT holder will not run correctly in a CAT spindle. If you are unsure, send us the machine make and model and we will confirm it.
ER collet chuck or hydraulic chuck for finishing?
Hydraulic, in almost every case. An ER system typically runs around 0.01 mm and its accuracy degrades as collets wear, while a hydraulic chuck holds 0.003 mm or better and damps vibration through the fluid chamber. The trade is cost and flexibility: one ER holder covers a wide diameter range, a hydraulic chuck does not. Many shops keep ER for roughing and drilling, and hydraulic for the finishing pass.
What runout can I actually expect?
Across the range, 0.003 mm to 0.01 mm depending on series. That is the holder on its own. Measured runout at the cutting edge also includes spindle condition, taper cleanliness, the tool shank tolerance and clamping torque, so a 0.003 mm holder in a dirty taper will not give you 0.003 mm at the tip.
Do I need balanced holders?
Above roughly 8,000 rpm it starts to matter, and above 15,000 rpm it is not optional. Our hydraulic chucks are balanced to G2.5 per ISO 1940 with residual unbalance of 1 g.mm or less, rated to 25,000 rpm on BT30 and BT40 and 20,000 rpm on BT50.
Can you supply non-standard gauge lengths or clamping diameters?
Yes. Non-standard reach, clamping diameter and coolant arrangements can be ground to order. Send the drawing or describe the interference you are working around and we will quote against it.
What do you need from me for a quote?
Four things get you a firm answer quickly: the spindle interface (BT40, CAT50, HSK-A63 and so on), the tool shank diameter, the reach or gauge length you need, and the operation – roughing, finishing, reaming or boring. Machine make and model helps if you have it.
Request a quote for tool holders