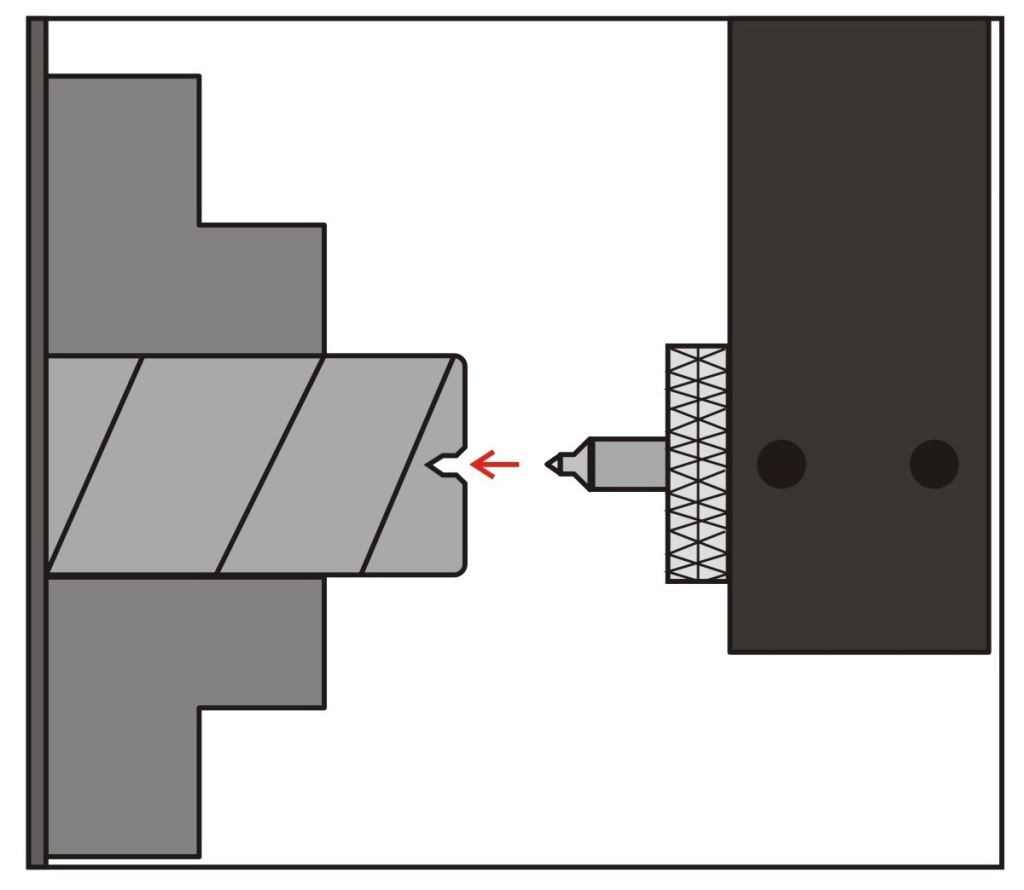
The Boring Bar Side Holder is a boring bar holder designed for mounting internal turning tools in a horizontal (side-mount) orientation, ideal for CNC lathes and turning centers where vertical clearance is limited.
Specification
- Supported Tool Diameters: Ø12 / Ø16 / Ø20 / Ø25 mm (other sizes available on request)
- Mounting Orientation: Horizontal / Side-mount configuration
- Clamping Method: Threaded locking screws (standard M6, M8 depending on model)
- Material: Hardened alloy steel or tool steel
- Surface Treatment: Black oxide coating or custom finishes
- Application: Internal boring, facing and grooving, fine-finishing in hard-to-reach areas
- Customization: tool bore size, overall dimensions, mounting hole position and thread size
Side-Mount vs Other Boring Bar Holders
How the bar is mounted on the turret decides whether you can reach into the bore at all, and whether it chatters once you do. The table below compares the common mounting methods.
| Holder type | Mounting | Height used | Clamping rigidity | Best suited to | Watch out for |
|---|---|---|---|---|---|
| Side-mount holder | Horizontal, clamped from the side | Low | Medium-high | Limited turret clearance, multi-station setups, confined-area boring | Torque the locking screws evenly; excess bore clearance turns straight into chatter |
| Standard top-clamp holder | Clamped from above | High | High | General internal turning with room to spare | Needs clearance above the turret |
| Boring bar sleeve | Bar slides into a sleeve, then clamped | Depends on the holder | Medium-high | Fitting a small bar into a larger holder bore | One more mating surface – the size has to be right or concentricity suffers |
| Spring collet sleeve (e.g. AEF) | Slotted body contracts elastically around the bar | Depends on the holder | High | Where concentricity and clamping rigidity matter most | Bar cylindricity must be good and sizes must match |
Bar Diameter and Recommended Overhang
| Bar diameter | Typical bore from | Steel bar (approx. 4xD) | Carbide bar (approx. 7xD) | Anti-vibration bar (approx. 10xD) |
|---|---|---|---|---|
| Ø12 mm | Ø16 mm and up | approx. 48 mm | approx. 84 mm | approx. 120 mm |
| Ø16 mm | Ø20 mm and up | approx. 64 mm | approx. 112 mm | approx. 160 mm |
| Ø20 mm | Ø25 mm and up | approx. 80 mm | approx. 140 mm | approx. 200 mm |
| Ø25 mm | Ø32 mm and up | approx. 100 mm | approx. 175 mm | approx. 250 mm |
Controlling Chatter in Internal Turning
- Shorten the overhang before anything else. Deflection scales with the cube of the overhang, so taking 20% off the extension roughly doubles the stiffness.
- Torque the locking screws evenly. Over-tightening one screw pushes the bar off centre, and once concentricity is gone nothing downstream will fix it.
- Fit matters more than finish. Any play between bore and bar gets amplified into chatter marks during the cut.
- Keep the nose radius smaller than the depth of cut. Excess radial force is the most common hidden cause of chatter when boring.
- At the limit, change material. When a steel bar can no longer cope, moving to carbide or an anti-vibration bar beats grinding the speed down further.
Datasheets
- Boring Bar Side Holder datasheet (PDF)
- Boring Bar Sleeve datasheet (PDF)
- Boring Bar Sleeve D16 datasheet (PDF)
- Mini Boring Bar Sleeve datasheet (PDF)
- Anti-Vibration Boring Bar datasheet (PDF)
- Browse all datasheets
Frequently Asked Questions
When should I use a side-mount boring bar holder?
The typical case is a turret with not enough vertical clearance, where a standard holder would interfere. Mounting the bar horizontally and clamping from the side lowers the height a single station occupies, which matters on multi-station setups and smaller turning centres. The other case is boring or grooving inside a confined area of the part, where you need every millimetre of clearance you can get.
Is a side-mount holder less rigid than a standard one?
Not meaningfully, provided the locking screws are the right count and torque and the bar-to-bore fit is correct. What actually drives vibration is the overhang and the bar material, not the clamping direction. In practice, shorten the overhang first and worry about everything else after.
How far can I extend the bar before it chatters?
Use diameter multiples as a starting point: roughly 4x diameter for a steel bar, 7x for carbide, and 10x for an anti-vibration bar. Beyond that, reduce depth of cut and feed, or move up to an anti-vibration bar.
Can you customise the mounting hole position and thread?
Yes. Tool bore size, overall dimensions, mounting hole position and thread size can all be made to drawing. Send us the turret interface drawing or dimensioned photos of the holder you currently use and we will confirm compatibility.
I have persistent chatter when boring – should I change the bar or the holder?
Check three things first: overhang length, the clearance between bar and bore, and whether the locking screws are torqued evenly. If all three are clean and chatter remains, then move from a steel bar to carbide or an anti-vibration bar. Doing it the other way round often means spending money with the problem still there.
What do you need from me for a quote?
Four things: turret specification and available clearance, the bar diameter you plan to use, the operation (boring, facing, grooving, finishing), and whether you need the mounting holes and thread made to drawing. We will confirm compatibility and come back with pricing and lead time.
Request a quote for boring bar holders