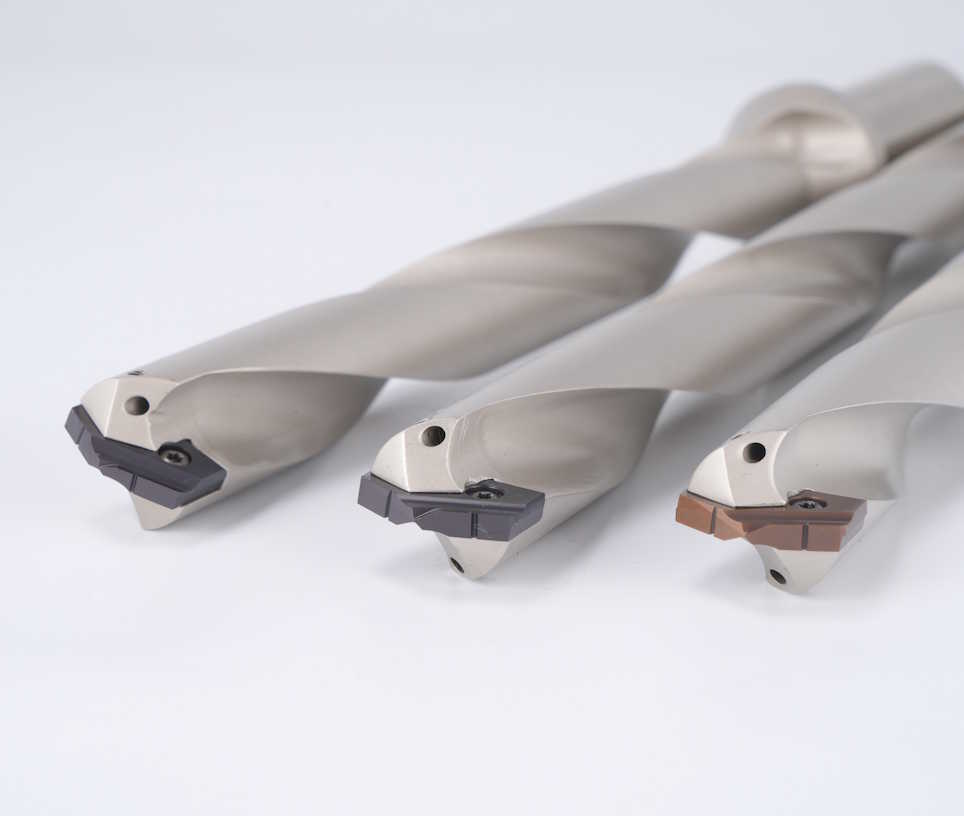
The Spade Drill is a modular, indexable drilling solution engineered for large-diameter and deep-hole machining. With a universal drill body and a selection of interchangeable insert types, it provides superior flexibility, lower tooling cost, and simplified inventory management. Available with carbide, powder high-speed steel (PM-HSS), and cobalt high-speed steel (HSS-Co) inserts.
Specification
- Insert Material Options: Carbide / Powder HSS / Cobalt HSS
- Insert Diameter Range: Ø9.5 mm – Ø114 mm
- Feed Rate Capability: 0.2 – 0.6 mm/rev
- Surface Speed (Vc): HSS 20-40 m/min; Carbide 60-80 m/min
- Drill Body Coolant: Central coolant hole, compatible with high-pressure internal coolant
- Insert Features: Chipbreaker groove, self-centering, double-edge cutting
- Machine Compatibility: Vertical drills, CNCs, rocker arm drills (HSS types preferred)
- Best Use Case: Deep-hole drilling, large-diameter boring, interrupted cuts
Product Content
The insert design features a chipbreaker groove for easy chip evacuation, a self-centering geometry for stable deep-hole drilling, and symmetrical cutting edges that minimize deflection. A separated drill body and insert design allows one drill body to handle multiple tasks by swapping insert materials to suit workpiece and machine rigidity – use HSS or powdered HSS inserts on lower-rigidity machines to prevent chipping of carbide inserts.
Spade Drill vs U-Drill vs Solid Carbide: Which to Use
Once the hole gets large or the machine gets old, choosing the wrong drilling method shows up as chipped inserts and scrapped parts. The table below puts the common options side by side so you can narrow things down before asking for a quote.
| Method | Typical diameter | Depth-to-diameter | Tooling cost structure | Best suited to | Watch out for |
|---|---|---|---|---|---|
| Spade drill | Ø9.5 – Ø114 mm | High, with pecking | One-off body cost, then inserts only | Large diameters, deep holes, interrupted cuts | Chip evacuation decides everything; drop to HSS inserts on less rigid machines |
| Indexable (U) drill | approx. Ø12 – Ø60 mm | Usually 3 – 5D | Body plus inner and outer inserts | Mid-range diameters, high-volume production | Needs higher speed and reliable through-coolant |
| Solid carbide drill | approx. Ø1 – Ø20 mm | 3 – 12D by series | Whole tool is consumable, regrindable | Small diameters, tight tolerance | High unit price; one crash is expensive |
| HSS twist drill | Ø1 – Ø50 mm | Usually 3 – 5D | Lowest | Older machines, one-offs and small batches | Slow; large diameters need pilot holes |
| Boring | Depends on the bar | Depends on overhang | Bar plus inserts | Finishing diameter and roundness | Finishes only – you still need an existing hole |
Starting Cutting Conditions
| Insert material | Cutting speed Vc | Feed f | Use when |
|---|---|---|---|
| Cobalt HSS (HSS-Co) | 20 – 30 m/min | 0.2 – 0.4 mm/rev | Older machines, radial arm drills, lower rigidity |
| Powder HSS (PM-HSS) | 25 – 40 m/min | 0.3 – 0.5 mm/rev | Balance of toughness and wear resistance, interrupted cuts |
| Carbide | 60 – 80 m/min | 0.3 – 0.6 mm/rev | Rigid CNC machines with stable through-coolant |
Chip Evacuation and Coolant in Deep Holes
- Always use through-coolant. The central hole in the body exists to flush chips up from the bottom. Past roughly 1.5x diameter, external flood does almost nothing.
- Peck beyond 3x diameter. Retracting in steps prevents chip packing and the re-cutting that follows it.
- No pilot hole needed. The self-centring insert geometry keeps walk to a minimum, so you can drill straight in.
- Reduce feed at breakthrough. The exit face is where the insert corner chips – halve the feed for the last 2 to 3 mm.
- Angled or curved entry: reduce speed and feed until the full edge is engaged, then return to normal conditions.
- Cast iron and other short-chipping materials can run on compressed air; steel should always be cut with coolant.
Datasheets
Frequently Asked Questions
What is the difference between a spade drill and an indexable (U) drill?
Two things: how the insert is held, and the diameter range. A U-drill uses two indexable inserts splitting the inner and outer cut, typically Ø12 to Ø60 mm, and relies on high spindle speed. A spade drill uses a single insert spanning the full diameter, reaches Ø114 mm, and the same body accepts carbide, powder HSS or cobalt HSS inserts. For large holes, older machines or interrupted cuts, a spade drill is usually the better economics.
How deep can a spade drill go?
It depends on body length and on how well chips clear. In practice, past about 3x diameter we recommend peck drilling and confirming that coolant actually reaches the cutting edge. Deep-hole failures are almost never about cutting power – they are about chips that cannot get out.
Do I need through-coolant?
Strongly recommended. The central coolant hole exists to flush chips up from the bottom of the hole. External flood has very little effect once the hole is deeper than roughly 1.5x diameter. Short-chipping materials such as cast iron can run on compressed air, but steel should always be cut with coolant.
My inserts chip quickly – what is usually causing it?
Three common causes. First, insufficient machine or holder rigidity – switching from carbide to powder HSS or cobalt HSS inserts usually fixes this immediately. Second, chips that are not clearing and get re-cut. Third, full feed maintained through breakthrough, which chips the corner on the exit face. Reduce feed by half when starting on an angled or curved surface as well.
Can I run this on an older radial arm drill?
Yes, but choose HSS or powder HSS inserts and stay at the low end of the speed range, around 20 to 30 m/min. Carbide inserts need stable speed and rigidity; on an older machine they tend to chip and end up costing more.
What do you need from me for a quote?
Five things: hole diameter, hole depth, workpiece material and hardness, machine type (spindle power, maximum speed, through-coolant or not), and expected quantity. We will recommend the body size and insert material, and come back with cutting condition suggestions, pricing and lead time.
Request a quote for spade drills