Our indexable end-face milling cutter heads are purpose-built for the H-beam and box-beam end-facing machines used throughout structural steel fabrication. Steel fabricators mount these rotating cutter heads on beam-end milling machines to face and bevel the web and flange ends of H-beams, turning rough flame-cut or sawn edges into clean, accurately angled surfaces so beam sections can be joined with full-penetration groove welds. As a trading company working directly with experienced Taiwanese toolmakers, we supply both the cutter heads and matching insert sets as complete, ready-to-run systems for beam-line equipment builders and steel fabrication shops worldwide.
Cutter Head Styles
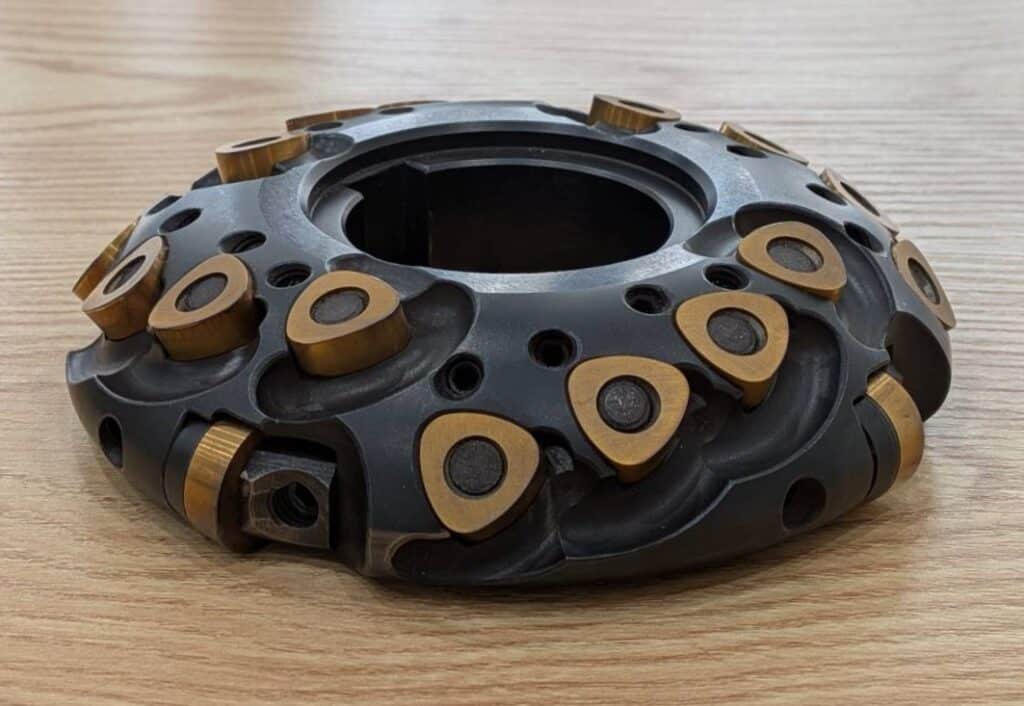
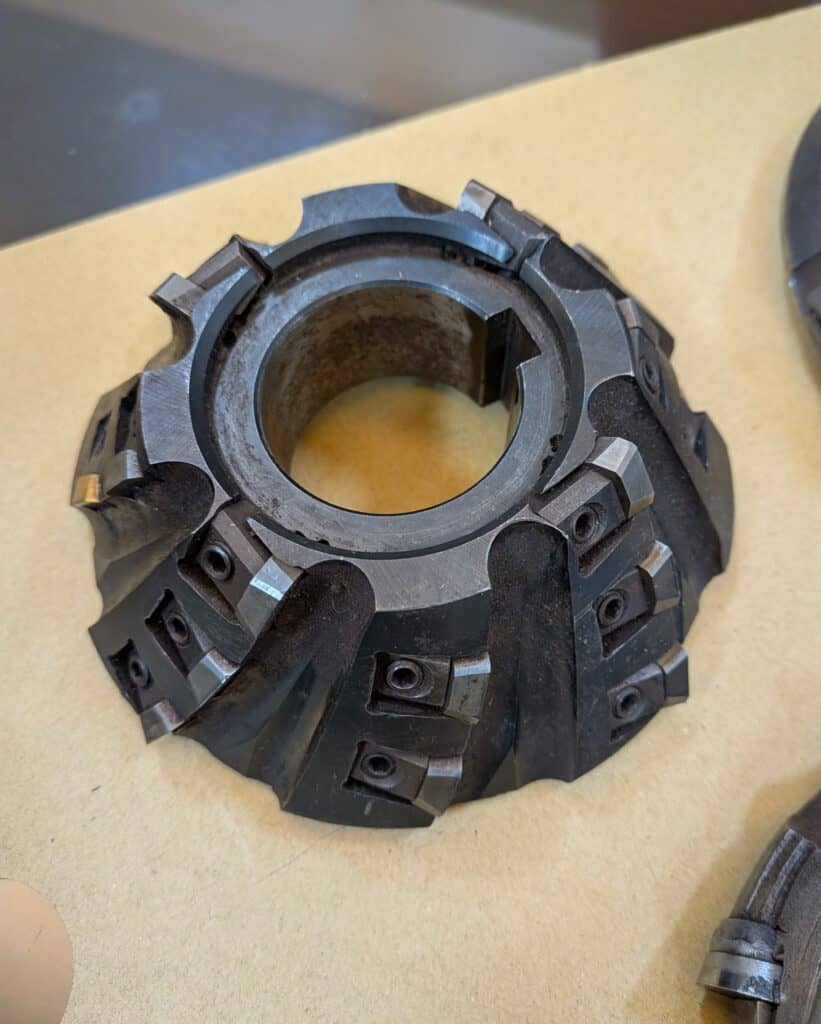
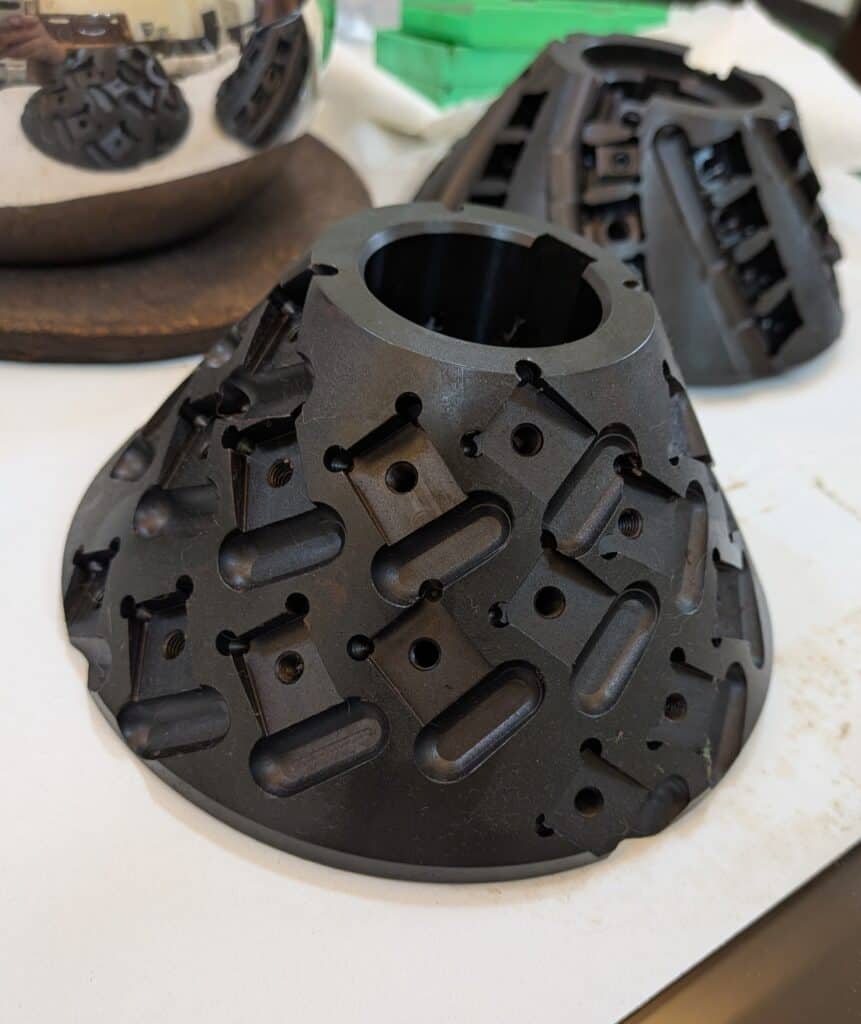
We offer two core cutter head styles to match different end-facing operations on H-beam and box-beam end-milling machines. The flat, shell-mount style cutter head features a large center bore and keyway for secure spindle mounting, distributing twelve to twenty-four insert pockets around its circumference for fast, square facing of the web and flange ends. The tapered, cone-profile cutter head tilts naturally into the beam edge, letting the machine’s milling head incline up to 45 degrees to cut the Y, X, K, and U bevel profiles required for full-penetration weld joints on heavier structural sections.
Insert Systems
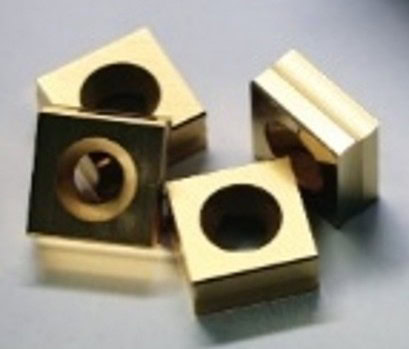
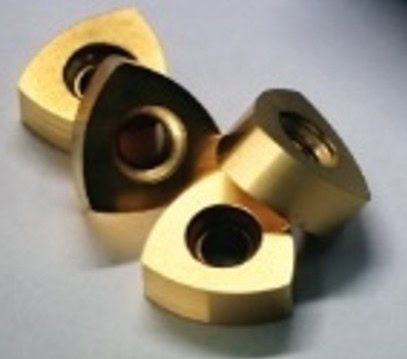
Both cutter head styles accept gold, titanium-nitride coated indexable inserts in square and round or trigon profiles. The square-style inserts hold a sharp, defined edge well suited to facing flat web and flange surfaces square, while the round and trigon inserts spread cutting load across a curved edge for smoother engagement when cutting bevel transitions and biting through heavier scale left over from flame cutting or sawing. Each insert is ground to tight tolerances so that any pocket position produces a consistent cutting circle, keeping the finished beam end flat, square, and ready for fit-up and welding.
Engineering & Quality Control
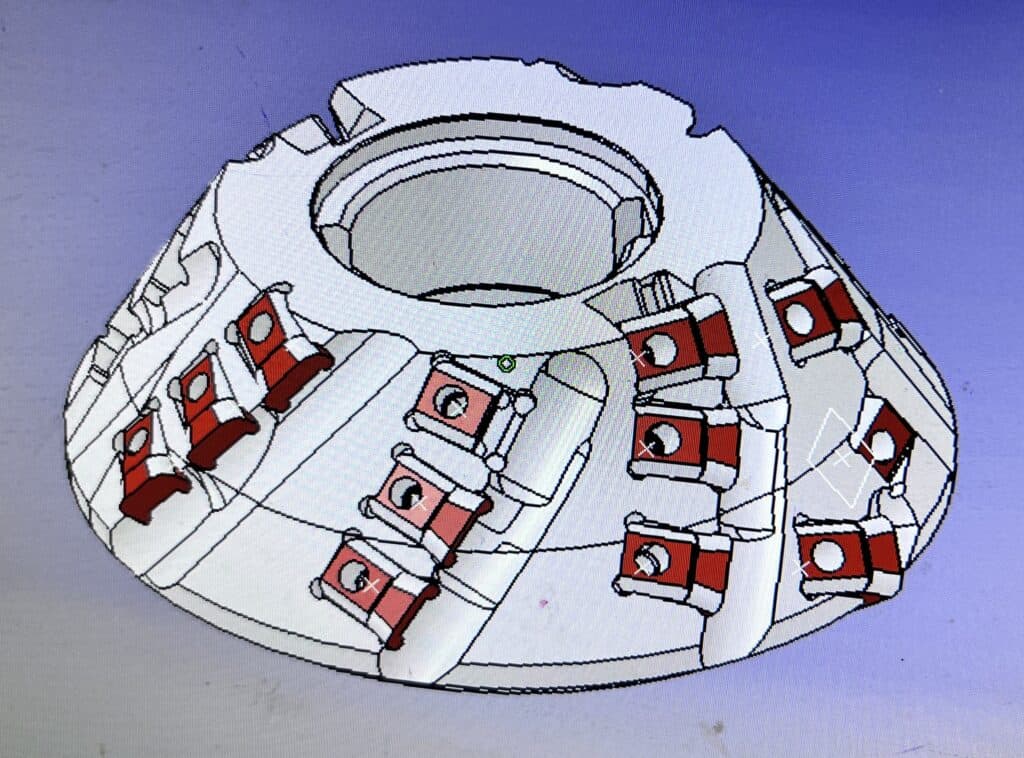
Every cutter head begins as a CAD-modeled design that maps out insert pocket angles, seating faces, and clamping screw positions before a single part is cut. This upfront engineering keeps the pockets in tight positional relation to one another, so the assembled cutter head runs true on the beam-end milling machine’s spindle with minimal vibration. We work with our partner factories to review these layouts and confirm dimensional accuracy before production, giving fabricators confidence that every beam end comes off the machine flat, square, and within the tolerance needed for a sound weld.
Specification
- Cutter Head Styles: flat shell-mount facing heads and tapered bevel-cutting heads
- Insert Pocket Count: 12 to 24 inserts, depending on cutter head diameter
- Insert Profiles Supported: square-style and round or trigon-style indexable carbide inserts
- Coating: gold titanium-nitride (TiN) coating for wear resistance and reduced cutting heat
- Mounting: keyway-drive center bore compatible with H-beam and box-beam end-face milling machines
- Applications: end-face facing and bevel milling (Y, X, K, and U profiles) of H-beams, box-beams, and other structural steel sections for full-penetration weld joint preparation
Product Content
As your sourcing partner, we handle everything from cutter head selection to insert grade matching, packaging, and export documentation, so beam-line equipment builders and steel fabricators can equip their end-facing machines with a reliable cutting solution under their own brand. Custom pocket counts, bore sizes, and insert geometries are available for OEM and private-label programs, and we can supply sample cutter heads for trial runs before committing to full production orders.